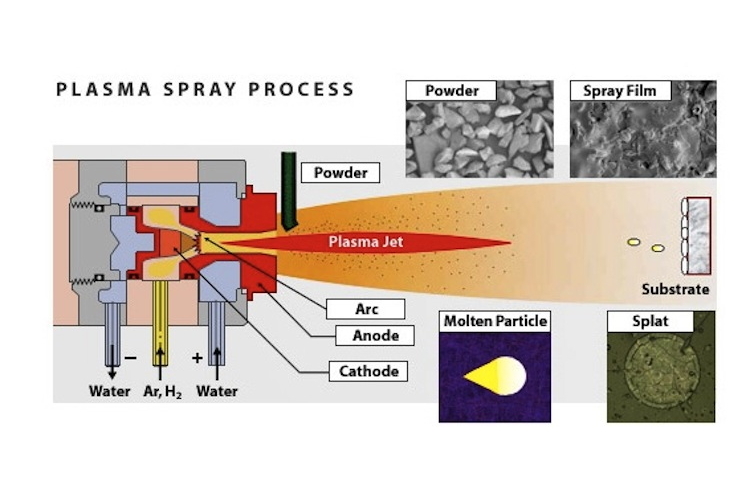
 A
plasma spray torch includes nitrogen, hydrogen, or helium in some
cases, is permitted to stream between a water-cooled copper anode
and a tungsten cathode. An electric arc is started between the two
anodes through a high recurrence release and is then managed to
utilize a powder. The arc ionizes the gas, making high-pressure
plasma. The subsequent increment in gas temperature, which may
surpass 30,000°C, thus expands the gas volume and consequently its
pressure and speed as it leaves the nozzle. Gas speed, which may be
supersonic, must not be taken as molecule speed. In plasma splash
torch the power level range from 30 to 80 kW, reaching as big as 120
kW. Argon is generally picked as the foundation gas because it is
chemically inactive and has great ionization qualities. Including the
diatomic gasses, hydrogen or nitrogen can build the gas enthalpy. The
powder is generally brought into the gas flow either simply outside
the light or in a separating way out locale of the nozzle (anode).
The powder is warmed and quickened by the high-temperature,
high-speed gas plasma flow. Torchworking parameters and design are
vital in deciding the speed and temperature achieved by the powder
molecules. The working items incorporate not just gas stream, power
level, powder feed rate, and bearer gas flow, additionally the
separation from the substrate (standoff) to the torch and the
deposition angle. The standoff is of significant importance because
satisfactory separation must be accommodated warming and quickening
the powder, yet excessive separation will permit the powder to cool
and lose speed as the gas stream is quite chilling and moderating
off. The size and morphology of powder particles affects the rate of
warming and speeding up and thus, the effectiveness of testimony and
covering quality. As often as possible, a to some degree higher cost
for powder with more tightly size appropriation is more than adjusted
for by the enhanced deposition effectiveness. Powder speeds as plasma
splash deposition range from around 300 to 550 m/s. Temperatures are
frequently at the melting point or marginally above. By and large,
higher temperatures and molecule speeds over the melting point
however without extreme super-heating, yield coverings with the most
astounding densities and bond qualities.
Tuesday, 17 September 2019
Plasma Spray
A
plasma spray torch includes nitrogen, hydrogen, or helium in some
cases, is permitted to stream between a water-cooled copper anode
and a tungsten cathode. An electric arc is started between the two
anodes through a high recurrence release and is then managed to
utilize a powder. The arc ionizes the gas, making high-pressure
plasma. The subsequent increment in gas temperature, which may
surpass 30,000°C, thus expands the gas volume and consequently its
pressure and speed as it leaves the nozzle. Gas speed, which may be
supersonic, must not be taken as molecule speed. In plasma splash
torch the power level range from 30 to 80 kW, reaching as big as 120
kW. Argon is generally picked as the foundation gas because it is
chemically inactive and has great ionization qualities. Including the
diatomic gasses, hydrogen or nitrogen can build the gas enthalpy. The
powder is generally brought into the gas flow either simply outside
the light or in a separating way out locale of the nozzle (anode).
The powder is warmed and quickened by the high-temperature,
high-speed gas plasma flow. Torchworking parameters and design are
vital in deciding the speed and temperature achieved by the powder
molecules. The working items incorporate not just gas stream, power
level, powder feed rate, and bearer gas flow, additionally the
separation from the substrate (standoff) to the torch and the
deposition angle. The standoff is of significant importance because
satisfactory separation must be accommodated warming and quickening
the powder, yet excessive separation will permit the powder to cool
and lose speed as the gas stream is quite chilling and moderating
off. The size and morphology of powder particles affects the rate of
warming and speeding up and thus, the effectiveness of testimony and
covering quality. As often as possible, a to some degree higher cost
for powder with more tightly size appropriation is more than adjusted
for by the enhanced deposition effectiveness. Powder speeds as plasma
splash deposition range from around 300 to 550 m/s. Temperatures are
frequently at the melting point or marginally above. By and large,
higher temperatures and molecule speeds over the melting point
however without extreme super-heating, yield coverings with the most
astounding densities and bond qualities.
Friday, 13 September 2019
Cold Pressure Welding
(a) the difference on a micro-scale of the local plastic strain occurring on matching opposite faces of the weld interface
(b) relative hardness of the metal and its oxide film, and
(c) mechanical properties of the oxide.
The second stage involves:
(a) plastic flow of the metal to the over-lapped areas; the stress at which this can take place is influenced by the stacking fault energy of the metal
(b) some relative shear displacement at the points where metal cleaned of oxide comes into contact; this is influenced by surface roughness Cold pressure welding is used for joining of aluminium cables, various kitchen furniture, electrolysis cells, communication lines, for joining wires and rods, production of heat exchangers at coolers and application of joining different materials nowadays. Various researchers carried some of the studies about cold pressure welding out: gave knowledge about investigations on pressure welding and cold pressure welding. [3] Investigated the mechanism of solid-state pressure welding. Examined the bonding mechanism of cold pressure welding. [5] Investigated cold pressure welding of aluminium and copper by butt upsetting. [6] Investigated effects on welding strength of process parameters in cold pressure welding of aluminium. [7] Obtained the surface roughness depending on welding strength in cold pressure welding of aluminium. [8] Directed the process parameters optimization for obtaining high weld strength in cold solid-state joining of sintered steel and copper powder metallurgical performs. The knowledge about the cold pressure welding method and the developments in its applications were given in this study. Then, as for example, cold pressure welding was applied on commercial purity aluminium alloy sheets as lap welding. 150 metric ton hydraulic press was used for the welding process. Before welding, the wire-brushing process was applied for preparing aluminium sheets, which are test parts, the roughness was determined with surface roughness equipment and afterwards, deformation was applied at different deformation ratios. Then, the microstructure of the welded parts at a given welding deformation was examined, and it was researched that whether joints were properly obtained or not. Then, the results were commented.
Tuesday, 3 September 2019
What is RT?
RT
is a volumetric examination method used for examining the entire
specimen rather than just the surface. It is the historical
approach to examine completed welds for surface and
subsurface discontinuities. The method uses the change in
absorption of radiation by solid metal and areas of a
discontinuity. The radiation transmitted reacts with the film, a
latent image is captured, and when the film is processed (developed)
creates a permanent image (radiograph) of the weld. Some methods are
available which use electronics to create a digital image and are
referred to as “filmless.” Due to the hazard of radiation, and
the licensing requirements, the cost can be higher and the trained
and certified personnel more limited, than with other NDE methods. An
NDT examiner interprets and evaluates the radiographs for differences
in absorption and transmission results. Radiographic indications show
a different density in comparison with the normal background image of
the weld or part being inspected. The radiographer also makes sure
that the film is exposed by the primary source of the radiation and
not backscatter radiation. The NDT examiner that performs the film
interpretation, evaluation and reporting should be certified as a
minimum to ASNT Level II requirements. However, all personnel
performing radiography are required to attend radiation safety
training and comply with the applicable regulatory requirements. There
are very specific requirements about the quality of the produced
radiograph, including the sharpness of the image, the ability to
prove adequate film density in the area of interest and sensitivity
to the size and type of expected flaws. The requirements include:
- Method to determine if backscatter is present.
- Permanent identification, traceable to the component.
- Film selection under SE-1815.
- Different designations for hole or wire-type image quality indicators (penetrameters).
- Suggested radiographic techniques.
- Facilities for viewing radiographs.
Calibration (certification of source size). The exposure and processing of a radiograph are considered acceptable when it meets the required quality features in terms of sensitivity and density. These factors are designed to ensure that imperfections of a dimension relative to section thickness will be revealed. Standards for industrial radiography require the use of one or more image quality indicators (IQIs) to determine the required sensitivity is achieved. The IQI that was previously known as penetrameter is no longer being used in most codes. To assess sensitivity the required hole or wire as specified by the governing code must be visible on the finished radiograph. Mistakes with IQIs (penetrameters) can have a much greater impact on thinner wall pipe where large root pass imperfections can significantly reduce the strength and integrity of a weld. IQIs (penetrameters) are tools used in industrial radiography to establish the quality level of the radiographic technique
Wednesday, 28 August 2019
Casing
Drilling a well modifies the mechanical and hydraulic equilibrium of the rocks around the borehole. Periodically this equilibrium has to be restored, by inserting a good casing. The casing is a steel tube that starts from the surface and goes down to the bottom of the hole and is rigidly connected to the rocky formation using cement slurry, which also guarantees hydraulic insulation. The casing transforms the well into a stable, permanent structure able to contain the tools for producing fluids from underground reservoirs. It supports the walls of the hole and prevents the migration of fluids from layers at high pressure to ones at low pressure. Furthermore, the casing enables circulation losses to be eliminated, protects the hole against damage caused by impacts and friction of the drill string, acts as an anchorage for the safety equipment and, in the case of a production well, also for the Christmas tree. At the end of drilling operations, a well consists of a series of concentric pipes of decreasing diameter, each of which reaches a greater depth than the preceding one. The casing is a seamless steel tube with male threading at both ends, joined by threaded sleeve joints. The dimensions of the tubes, types of thread and joints are standardized (API standards). There are also Special direct-coupling casings, without a sleeve joint.
The functions and names of the various casings vary according to the depth. Starting from the uppermost and largest casing first comes the conductor pipe, then the surface casing and the intermediate casing, and finally the production casing. The first casing is called the conductor pipe and is driven by percussion to a depth normally of 30 to 50 m. It permits the circulation of the mud during the first drilling phase, protecting the surface unconsolidated formations against erosion due to the mud circulation, which could compromise the stability of the rig foundations. The conductor pipe is not inserted in a drilled hole and is not usually cemented, and therefore it is not considered a casing in the true sense of the word. The first casing column is next and protects the hole drilled inside the conductor pipe. It is also called the surface casing and its functions are to protect the freshwater aquifers against potential pollution by the mud, to provide anchorage for the subsequent casing, and to support the wellhead. To increase its stiffness and make it capable of bearing the compressive loads resulting from the positioning of the subsequent casings, the surface casing is cemented up to the surface. Its length depends on the depth of the aquifers and on the calculated well-head pressure following the entry of fluids from the bottom hole into the casing.
Friday, 16 August 2019
Wear Factors
 The wearing of metal parts is the gradual decay or breakdown of the metal. When a part becomes so deformed that it cannot perform adequately, it must be replaced or rebuilt. Though the end results of wear are similar, the causes of wear are different. It is essential to understand the wear factors involved before making a hard surfacing product selection. It is actually easy to select a surfacing alloy if all metal components are subjected to only one type of wear. However, a metal part is usually worn by combinations of two or more types of wear. This makes an alloy selection considerably more complicated. A hard surfacing alloy can thus be a compromise between each wear factor. The initial focus should centre on the primary wear factor and then the secondary wear factor(s) should be examined. For example: upon examining a worn metal part, it is determined the primary wear factor is abrasion and the secondary wear factor is a light impact. The surfacing alloy chosen should not only have a good abrasion resistance but also a fair amount of impact resistance. There are five major types of wear Abrasive (3 categories)
Impact
Adhesive
High temperature
Corrosive.
Abrasive wear - Abrasive wear is caused due to the foreign materials rubbing against a metal part. 50 - 60% of all wear on industrial metal components is due to this. Abrasive wear is this a wear problem. It can be categorized into three:
a. Low-stress scratching abrasion – This is the least severe type of abrasion where metal parts are worn away through the repeated scouring action of hard, sharp particles moving across a metal surface at varying velocities. The velocity, hardness, edge sharpness, angle of introduction and size of the abrasive particles all combine to affect the amount of abrasion.
b. High-stress grinding abrasion – this is more severe than simple scratching that results when small hard abrasive particles are forced against a metal surface with enough force that the particle is crushed, in a grinding mode. Most often the compressive force is supplied by two metal components with the abrasive sandwiched between the two - sometimes referred to as three-body abrasion. The surface becomes scored and surface cracking can occur.
Saturday, 3 August 2019
Valves
 The variety of valves available for use in piping systems is extensive. This is due to the range of functions that valves perform, the diversity of fluids carried, and the varying conditions under which valves must perform these tasks. Valves can be examined under the following headings:
● Basic parts
● Functions performed by valves
● Valve types
● Installation of valves
● Specification of valves.
The main structure of the valve is the body, which contains – or to which is attached – the other parts of the valve. The main structure must possess sufficient mechanical strength and sufficient resistance to corrosion, erosion and high temperature to meet service conditions. The material from which the valve body is made is important and common materials in use include carbon steel, low-alloy steel, bronze, brass, stainless steel. The operator is the method of actuating the valve. Valves may be operated manually: by the use of handwheels, levers and chains, by geared handwheels on larger valves or by powered operation employing electric, pneumatic or hydraulic actuators. Powered actuators are normally used when:
● Rapid opening or closing is required
● The valve is operated very frequently
● Access to the valve is difficult
● The operation of the valve requires great effort
● Valve operation presents a safety hazard.
Functions performed by valves
Valves perform the following basic functions.
● They shut off the supply in a pipeline or they enable a piece of the pipeline to be isolated so that repairs to piping or equipment can be carried out faulty or damaged items can be replaced, etc. This is shut-off or stops valve.
● The throttle, regulate or restrict the flow passing along a pipeline by partially closing the area of flow through the valve.
● They redirect the flow at a branch line by changing the path along which the flow occurs.
● They protect a system against excessive pressure or sudden increases in pressure. These are safety valves or relief valves. When the pressure in a line reaches a pre-set high pressure, the valve opens and allows the pressure to escape either to the atmosphere or to another part of the system. Safety valves are
the ones that are usually used for steam, air or other gases. Relief valves are usually used for liquids.
● They enable one part of a continuous system of piping to operate at a different pressure from another part. These are pressure-reducing valves (also known as pressure regulators) and are often used in air piping to reduce the compressor or mainline pressure down to a low value for operation of low- pressure equipment.
● They prevent flow in one direction along a pipe or they allow flow in one direction only. This valve is referred to as a non-return, or check or reflux valve.
Wednesday, 24 July 2019
Weld Cladding

Weld
cladding techniques were first developed at Strachan & Henshaw,
Bristol, United Kingdom, for use on defence equipment, especially,
for various parts of submarines. Through weld cladding, the composite
structure is developed by the fusion welding process. All metals used
as fillers may be used for weld cladding. Materials such as nickel
and cobalt alloys, copper alloys, manganese alloys, alloy steels, and
few composites are commonly used for weld cladding. Weld clad
materials are widely used in various industries such as chemical,
fertilizer, nuclear and steam power plants, food processing and
petrochemical industries. Various industrial components whose base
metals are weld-clad are steel pressure vessels, paper digesters,
urea reactors, tube sheets and nuclear reactor containment vessels.
Cladding using gas tungsten arc welding is widely used in aircraft
engine components to maintain high quality. Weld cladding can be done
by using various processes such as Submerged arc welding (SAW), Gas
metal arc welding (GMAW), Gas tungsten arc welding (GTAW), Flux-cored
arc welding (FCAW), Submerged arc strip cladding (SASC), Electro slag
strip cladding (ESSC), Plasma arc welding (PAW), Explosive welding,
etc. GTAW and PAW are widely used for the cladding operations, and
they produce superior quality cladding because they generate high
stable arc and spatter free metal transfer. Welding variables and
inert gas shielding can be precisely controlled in both GTAW and PAW.
Though GTAW and PAW cladding can produce excellent overlay with a
variety of alloy materials, deposition rate is low compared to
other processes which limit its application in industries. Submerged
arc strip cladding (SASC) and Electro slag strip cladding (ESSC)
is extensively used for cladding large surfaces of the heavy–wall
pressure vessels. Three most important characteristics of SASC and
ESSC are high deposition rate, low dilution and high deposition
quality. Deposition rate in ESSC is much more than in SASC because of
the absence of arc, whereas, dilution in ESSC is less compared to
SASC because of the same reason. Weld cladding is widely done using
flux-cored arc welding (FCAW) process due to various advantages. With
properly established process parameters automation and robotization
can be done easily in FCAW. Wear, corrosion and heat resistance of
material surface is enhanced by plasma transferred arc (PTA)
surfacing. PTA process is also considered as an advanced GTAW process
used largely for overlay applications. Various advantages of PTA
surfacing are very high deposition quality, high-energy
concentration, narrow heat-affected zone, less weld distortion, etc.
On the other side, demerits of PTA surfacing are low deposition
rates, overspray, and very high equipment costs Cladding with the use
of submerged arc welding (SAW) is applied for large areas, and its
fusion efficiency is quite high. SAW can be easily automated and
employed especially for heavy section work.
Subscribe to:
Posts (Atom)